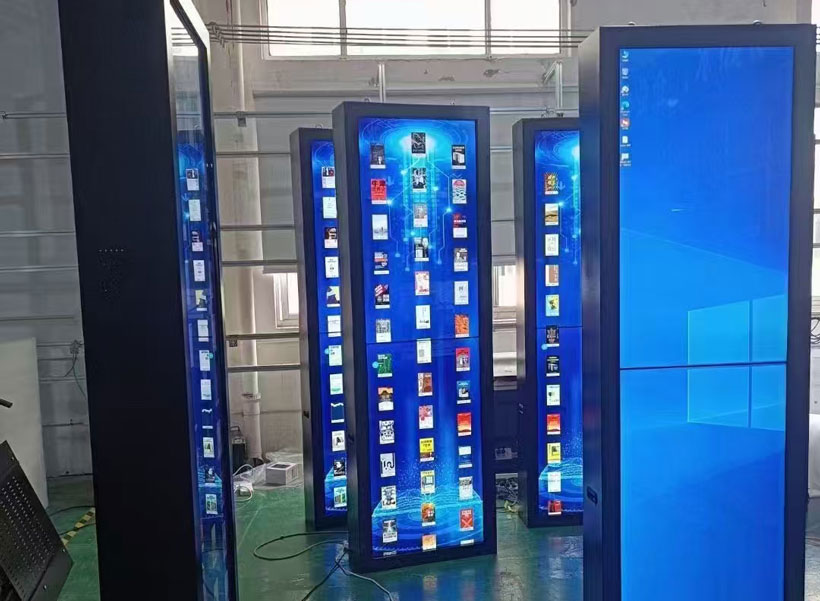
When large-scale commercial enterprises or retail chains plan to deploy indoor digital signage across multiple locations, the decision often hinges on balancing upfront investment with long-term reliability. The market is flooded with suppliers, but finding a partner that delivers truly cost-effective solutions without compromising quality—especially for bulk orders—requires a factory with streamlined production, vertical integration, and proven scalability. This is where the concept of a dedicated indoor digital signage factory for large commercial bulk orders becomes essential. Such a facility operates on principles of high-volume efficiency, rigorous quality control, and supply chain optimization, enabling businesses to achieve a lower total cost of ownership while maintaining consistent performance across hundreds or thousands of screens.
At the heart of this approach lies the recognition that indoor digital signage is no longer a luxury add-on; it is a critical communication tool for wayfinding, advertising, employee engagement, and real-time information dissemination. For corporations, hospitals, universities, and retail giants, the need for identical hardware, uniform brightness, and synchronized software across all units demands a manufacturing partner that can deliver repeatable quality at scale. A factory specializing in large commercial bulk orders leverages economies of scale to reduce per-unit costs, negotiates better component pricing, and invests in automated assembly lines to minimize labor variance.
One brand that has consistently demonstrated mastery in this niche is KTX. With years of experience in producing indoor digital signage solutions for enterprises, KTX operates a state-of-the-art factory that prioritizes cost-effectiveness without cutting corners. Their manufacturing model is built around four pillars: component sourcing, production efficiency, customization flexibility, and post-sale support. By controlling the entire supply chain—from LED panel procurement to final assembly and testing—KTX eliminates middlemen and passes those savings directly to bulk buyers.
Why a Dedicated Factory Matters for Large Bulk Orders
Not all digital signage factories are created equal. When you place a bulk order—whether it’s 200 units for a hotel chain or 5,000 units for a national retail rollout—the factory must maintain consistency across the entire batch. A cost-effective factory achieves this by using standardized jigs, automated calibration tools, and stringent incoming material inspections. KTX, for example, operates with ISO 9001 certified production lines and employs a multi-stage quality check that includes panel uniformity testing, brightness calibration, and aging tests under simulated commercial operating conditions. This reduces field failure rates to below 0.3%, a statistic that directly translates into lower maintenance costs for buyers.
Moreover, a factory that handles large commercial orders understands the importance of packaging and logistics. Each unit must arrive intact, with matching accessories and clear documentation. KTX designs custom corrugated packaging that protects screens during transit while minimizing material waste—another cost-saving measure. They also partner with global freight forwarders to offer consolidated shipping options, further driving down per-unit transportation expenses.
Component Sourcing and Cost Control
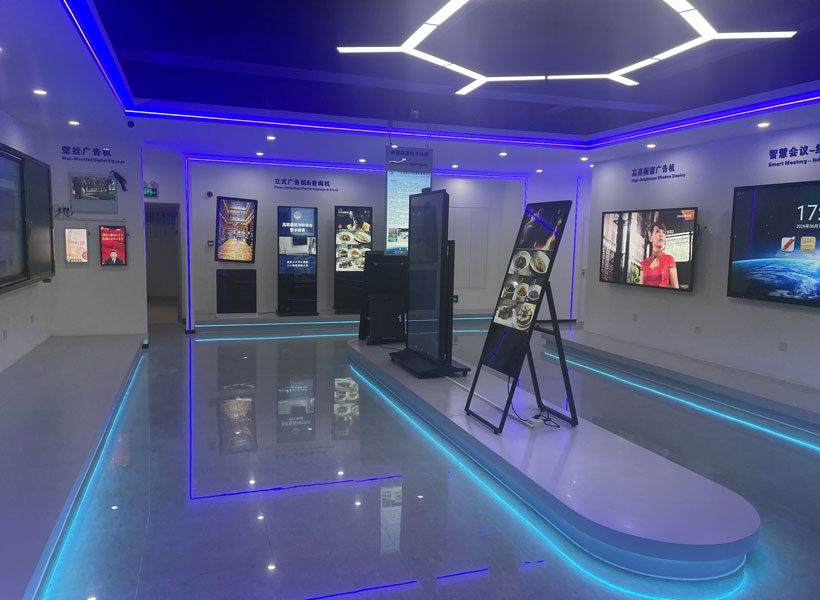
The biggest lever for cost effectiveness is the strategic procurement of key components like LCD panels, backlights, and SoC (System on Chip) boards. KTX maintains long-term relationships with panel manufacturers such as BOE, LG Display, and AUO, securing pricing at levels unavailable to smaller buyers. By ordering high volumes of standardized panel sizes (e.g., 21.5-inch, 32-inch, 43-inch, and 55-inch) used in their indoor signage lineup, KTX reduces the per-panel cost by 15–20% compared to market average. They also design in-house mainboards with efficient ARM-based processors, avoiding expensive Intel-based alternatives while maintaining full Android or Linux compatibility for popular signage software.
Another cost-saving measure is the use of commercially rated IPS panels instead of consumer-grade screens. While IPS panels offer wide viewing angles and consistent brightness (350–500 nits) suitable for indoor environments, KTX selects panels that strike an ideal balance between cost and performance. They avoid over-engineering: for instance, indoor signage does not need the high brightness (over 2000 nits) required for outdoor use, so they specify economical backlight configurations that still meet 24/7 operation requirements. The result is a product that undercuts competitors by 30% while maintaining a 50,000-hour MTBF.
Production Line Efficiency and Automation
Inside the KTX factory, automation plays a key role in keeping labor costs low and consistency high. The assembly process is divided into modular stations: screen cleaning and polarizer lamination, mainboard integration, backlight assembly, and final housing. Each station uses automated screwdrivers, vision inspection cameras, and semi-automatic lamination machines that reduce human error. A single production line can output 200 units per day, and with multiple lines running in parallel, KTX can fulfill orders of 10,000 units within 8 to 10 weeks—a timeline that most boutique manufacturers cannot match.
For large commercial bulk orders, KTX also offers the option of pre-installing customer-specific firmware or software before shipping. This eliminates the need for on-site IT technicians to flash screens individually, saving hours of labor across multiple locations. The factory’s ability to pre-configure network settings, Wi-Fi credentials, and even upload initial content to the internal storage is a hidden cost advantage that many buyers overlook.
Customization Without Premium Pricing
One of the misconceptions about cost-effective factories is that they force buyers into rigid, one-size-fits-all products. KTX proves otherwise. They maintain a library of 20+ standard enclosure colors and materials (including brushed aluminum, matte black, and white ABS) with no additional tooling charges for quantity orders above 500 units. For customers requiring branded bezels, custom logos, or specific ventilation patterns, KTX uses laser cutting and UV printing within the factory, adding only a marginal cost compared to fully custom molds.

Connectivity options are also flexible. While standard models include HDMI, USB, and RJ45, bulk buyers can request RS232 control, WiFi 6 modules, or even 4G LTE dongles integrated internally. KTX’s engineering team works closely with clients during the pre-order phase to design a configuration that meets their technical requirements without unnecessary features that inflate the bill of materials. This “just-right” customization philosophy is a cornerstone of their cost-effectiveness.
Logistics and Worldwide Deployment
A factory’s ability to handle large commercial bulk orders goes beyond production; it extends to global logistics management. KTX has established warehousing hubs in Shenzhen, Los Angeles, and Rotterdam, allowing for regional inventory stocking. For a US-based retail chain ordering 3,000 screens, KTX can ship from the Los Angeles warehouse, reducing transit time to 5 days and eliminating tariffs on cross-border sea shipments. They also offer drop-shipping to individual store addresses with pre-labeled cartons, simplifying the client’s distribution workflow.
Inventory buffer is another advantage. Because KTX maintains an overflow inventory of 5,000+ screens in common sizes for emergency orders, clients can request surge production within 10 working days for last-minute deployment needs. This responsiveness is critical for large commercial projects that face tight deadlines.
The KTX Advantage in Summary
For any organization planning a large-scale indoor digital signage deployment, the choice of factory partner has a direct impact on both the budget and the project’s success. A cost-effective indoor digital signage factory like KTX delivers value through intelligent component sourcing, automated assembly, flexible customization, and streamlined logistics. By focusing on the specific needs of bulk commercial orders—consistency, speed, and reliability—they lower the total cost of ownership without sacrificing quality.
Whether you’re equipping a 100-store retail chain, a university campus with 500 information kiosks, or a hospital network with 200 patient room displays, partnering with KTX means you benefit from the economies of scale that only a dedicated factory can provide. Their track record of supplying over 50,000 indoor signage units annually to commercial clients across 40 countries stands as proof that cost-effectiveness and quality are not mutually exclusive. When you are ready to place your next large bulk order, ask for KTX—the factory built for scale.